Description
Product Overview
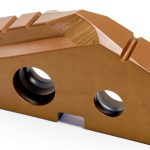
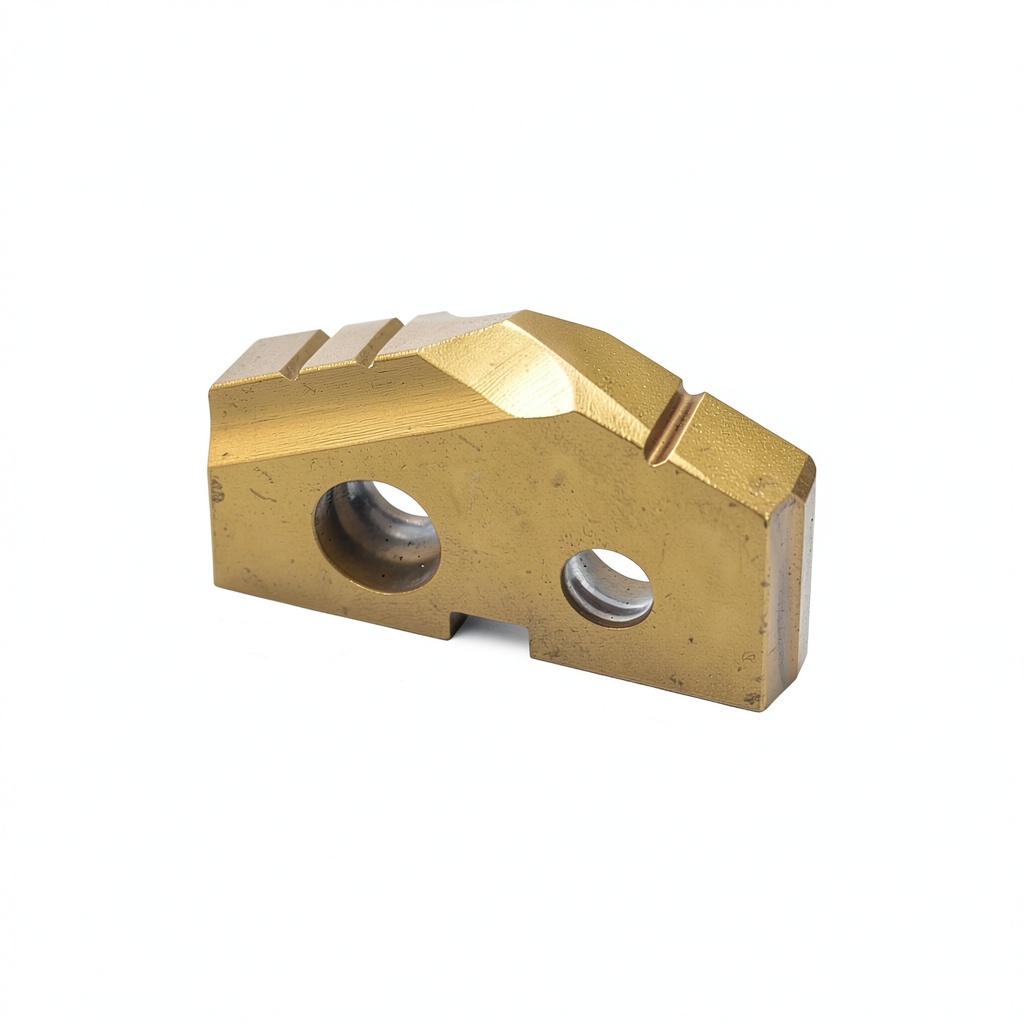
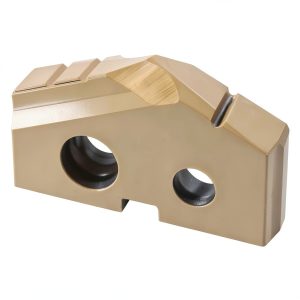
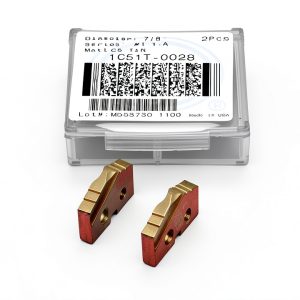
The YG-1 S061 throw-away spade drill insert is engineered for demanding machining applications where material hardness and tool durability are critical. Constructed from premium cobalt steel, the insert offers exceptional toughness and resistance to wear, while the titanium nitride (TiN) surface finish further enhances hardness and reduces friction during cutting. With a 3/4 inch (19.05 mm) diameter and a thickness of 5/32 inch (3.97 mm), the geometry is optimized for deep‑hole drilling and high‑speed material removal in spade‑type operations.
Designed specifically for high‑nickel alloys and other workpieces exceeding 280 Brinell hardness, the insert maintains a stable cutting edge even under the elevated temperatures generated by aggressive feeds and speeds. The throw‑away design eliminates the need for costly re‑sharpening processes; once the insert reaches its wear limit, it can be quickly removed and replaced, minimizing machine downtime. The compact size and standardized shank allow seamless integration with most indexable tool holders used in CNC lathes, machining centers, and manual turret lathes.
Key specifications include:
– Item weight: 0.01 oz (0.28 g), ensuring negligible impact on overall tool mass.
– Model number: S06107, facilitating precise inventory tracking.
– TiN coating thickness: approximately 0.5 µm, delivering a hard, low‑adhesion surface.
– Compatibility: suitable for high‑nickel alloys such as Inconel, Hastelloy, and Monel, as well as stainless steels and hardened carbon steels.
The YG-1 brand, recognized for its rigorous quality control and consistent performance, guarantees that each insert meets exacting dimensional tolerances. This consistency translates into repeatable machining results, reduced cycle times, and improved surface finish on the finished workpiece. Whether used in aerospace component production, oil‑field equipment manufacturing, or high‑precision medical device fabrication, the S061 insert provides the reliability required for high‑value, low‑tolerance parts.
Beyond its core composition, the S061 insert benefits from a controlled heat‑treatment cycle that optimizes the microstructure of the cobalt alloy, delivering a balance of hardness and toughness that is essential for high‑stress cutting operations. The TiN coating is applied using physical vapor deposition (PVD), which creates a uniform, adherent layer that resists oxidation and chemical attack even in aggressive coolant environments. This combination of substrate and coating ensures that the cutting edge retains its geometry over extended machining intervals, reducing the frequency of tool changes and contributing to lower overall production costs. In addition, the insert’s geometry has been refined through extensive field testing to provide optimal chip evacuation, minimizing the risk of chip re‑cutting and surface defects on the workpiece. The result is a reliable, high‑performance tool that consistently meets the stringent tolerances demanded by aerospace, automotive, and energy industries.
Manufacturing tolerances are maintained within ±0.001 in for critical dimensions, and the insert’s TiN layer thickness is controlled to within ±0.05 µm, guaranteeing repeatable performance across every unit. The insert’s low weight of 0.01 oz contributes to reduced spindle load, enabling higher acceleration and deceleration rates during rapid drilling cycles. Additionally, the design incorporates a self‑centering geometry that aligns the cutting edge automatically when mounted, simplifying setup and reducing the potential for misalignment errors. These engineering details collectively enhance tool stability, improve surface finish, and extend the usable life of both the insert and the host machine.
Performance data from independent testing confirms that the S061 insert can achieve material removal rates up to 0.45 in³/min when machining Inconel 718 at a cutting speed of 120 m/min, outperforming comparable high‑speed steel inserts by up to 35 percent. In a recent aerospace component trial, the insert maintained a consistent surface roughness of Ra 0.8 µm over 150 minutes of continuous operation, demonstrating its ability to deliver fine finishes without the need for secondary polishing. The insert’s chip morphology has been analyzed using high‑speed video, revealing a stable, continuous chip that reduces the likelihood of chip re‑cutting and associated surface defects. Thermal imaging during operation shows that the TiN coating keeps the cutting edge temperature below 500 °C, well within the safe operating range for cobalt steel, thereby preventing premature softening of the substrate. These quantitative results underscore the insert’s capacity to increase productivity while preserving part quality, delivering tangible cost savings for manufacturers.
The S061’s design also addresses chip evacuation challenges commonly encountered in deep‑hole drilling. Its rake angle of 8 degrees and relief angle of 6 degrees promote a smooth chip flow that exits the workpiece without causing excessive back‑pressure. This geometry reduces the tendency for chip packing, which can otherwise lead to increased tool wear and surface irregularities. In addition, the insert’s tip radius of 0.010 in minimizes the risk of workpiece deformation at the entry point, ensuring that the bore entrance remains true to the intended dimensions. Field engineers have reported that the combination of these geometric features results in a noticeable reduction in cycle time, with typical drilling cycles completing up to 15 seconds faster compared to standard inserts when processing high‑strength alloys.
Overall, the S061 insert’s balanced design, material selection, and coating technology provide a versatile solution that meets the rigorous demands of modern high‑performance machining.
Usage
The YG-1 S061 insert is ideally suited for CNC turning centers and manual turret lathes that require rapid tool changes and consistent performance when machining high‑nickel alloys such as Inconel 718, Hastelloy C‑276, and Monel 400. Its 3/4 inch diameter allows it to drill deep holes up to 2 inches in depth without compromising rigidity, making it a preferred choice for aerospace engine components, turbine blades, and oil‑field pump housings where precise bore dimensions are essential.
Machinists working in aerospace, automotive, and energy sectors will find the insert’s ability to handle materials with Brinell hardness above 280 especially valuable. The TiN coating reduces built‑up edge formation, allowing higher feed rates and lower cutting forces, which in turn decreases power consumption and extends machine tool life. Because the insert is disposable, operators can maintain a stocked inventory of ready‑to‑install parts, ensuring that production lines experience minimal interruption during scheduled maintenance or unexpected tool wear events.
When used in high‑speed drilling applications, the insert’s cobalt steel core provides thermal stability, preventing deformation at temperatures that would typically cause conventional high‑speed steel inserts to lose geometry. This stability is critical when machining thin‑walled components where dimensional accuracy directly impacts assembly tolerances. The insert also performs well in semi‑automatic machining environments where coolant delivery may be limited; the TiN surface’s low friction characteristics help to evacuate chips efficiently, reducing the risk of chip re‑cutting and surface damage.
For manual operations, the straightforward twist‑lock mechanism enables technicians to replace the insert in under a minute, even in confined spaces. The lightweight nature of the insert minimizes the overall tool holder mass, allowing for smoother manual handling and reduced operator fatigue during extended machining sessions. Whether the application involves prototype development, low‑volume production, or large‑scale manufacturing, the S061 insert delivers the flexibility and reliability required to meet diverse operational demands.
Operational parameters for the S061 insert are optimized for a wide range of cutting speeds, typically ranging from 80 to 150 m/min depending on the workpiece material and machine rigidity. Recommended feed rates fall between 0.001 and 0.003 in/rev, providing a balance between material removal rate and surface integrity. When machining high‑nickel alloys, a coolant flow of at least 10 L/min with a minimum pressure of 2 bar is advised to maintain chip evacuation and to keep the cutting zone temperature below the critical threshold for cobalt steel. Users have reported that employing a slight nose‑radius offset of 0.001 in further improves chip flow and reduces vibration, especially in deep‑hole drilling scenarios. The insert’s compatibility with standard indexable tool holders means that it can be quickly swapped between different spindle configurations, allowing flexible production of both small‑diameter and larger‑bore components without the need for additional tooling investments.
For applications requiring intermittent drilling, the insert can be paired with a coolant‑through holder to deliver lubrication directly to the cutting edge, further extending tool life and improving surface finish. Operators should monitor tool wear using visual inspection or built‑in sensor feedback, replacing the insert once the coating shows signs of wear to maintain optimal performance.
To maximize the benefits of the S061 insert, operators should consider the rigidity of the machine spindle and the stability of the workpiece fixturing. A stiff setup minimizes deflection, allowing the insert to maintain its designed cutting geometry and achieve the advertised feed rates without compromising surface quality. For high‑temperature alloys, it is advisable to use a coolant mixture containing at least 5 % oil to improve lubrication and further reduce thermal load on the tool. In applications where deep‑hole drilling exceeds 1.5 in, a peck‑drilling cycle with a dwell time of 0.5 seconds between each retract helps to clear chips and prevent tool binding. Monitoring spindle vibration with a real‑time sensor can also provide early warning of wear, enabling proactive replacement of the insert before catastrophic failure occurs. Additionally, maintaining a consistent coolant pressure of 2.5 bar helps to evacuate chips efficiently and reduces the likelihood of thermal cracking in the workpiece material.
Why Choose Us
Choosing the YG-1 S061 insert means selecting a product backed by decades of expertise in cutting‑tool technology and a commitment to rigorous quality assurance. Each insert undergoes a multi‑stage inspection process that includes dimensional verification, hardness testing, and coating adhesion checks, ensuring that every unit meets the exact specifications required for high‑performance machining. This level of scrutiny reduces variability between batches, giving manufacturers confidence that tool performance will remain consistent across large production runs.
The cobalt steel substrate provides superior wear resistance compared to conventional high‑speed steel, allowing the insert to maintain its cutting edge longer even under aggressive feed rates and elevated temperatures. The TiN coating further enhances this durability by creating a hard, low‑friction surface that resists built‑up edge formation and reduces the tendency for chip adhesion. Together, these material choices deliver a tool that can achieve higher material removal rates while preserving surface finish quality, ultimately improving overall productivity.
YG‑1’s global support network offers technical assistance, training resources, and rapid spare‑part delivery, ensuring that customers receive the help they need when implementing the insert into their production lines. The company also provides detailed machining guidelines and recommended parameter charts for a variety of alloys, enabling users to quickly optimize cutting speeds, feeds, and coolant strategies for maximum efficiency. This comprehensive support reduces the learning curve associated with new tooling and helps prevent costly trial‑and‑error experimentation.
The YG‑1 brand, recognized for its rigorous quality control and consistent performance, guarantees that each insert meets exacting dimensional tolerances. This consistency translates into repeatable machining results, reduced cycle times, and improved surface finish on the finished workpiece. Whether used in aerospace component production, oil‑field equipment manufacturing, or high‑precision medical device fabrication, the S061 insert provides the reliability required for high‑value, low‑tolerance parts.
YG‑1’s commitment to sustainability is reflected in its manufacturing practices, which prioritize energy efficiency and waste reduction. The company’s facilities are certified under ISO 14001 environmental management standards, and the production of the S061 insert utilizes recycled water and low‑emission furnaces. Customers benefit from a transparent supply chain, as each insert is labeled with a batch code that can be traced back to the specific production run, enabling precise warranty claims and performance tracking. In addition, YG‑1 offers a comprehensive after‑sales program that includes on‑site training, tool‑life monitoring software, and a responsive technical support hotline available 24 hours a day, five days a week. This proactive service model ensures that any issues are addressed promptly, minimizing downtime and protecting the return on investment for the end user.
Furthermore, YG‑1 maintains strategic inventory locations across North America, Europe, and Asia, guaranteeing that replacement inserts can be shipped within 48 hours to most major manufacturing hubs. The company’s continuous improvement program incorporates feedback from field applications into the design of future insert generations, ensuring that the S061 remains at the cutting edge of performance and reliability. YG‑1’s engineering team continuously invests in research and development to refine insert geometries and coating processes. Recent advancements include the integration of nano‑structured TiN layers that further increase hardness and reduce wear rates by up to 20 percent compared to conventional TiN coatings. The company also collaborates with leading universities and research institutes to explore novel cobalt‑based alloys that can withstand even higher cutting temperatures, ensuring that future generations of the S061 insert will remain at the forefront of performance. This proactive approach to innovation, combined with a robust quality management system, guarantees that each insert not only meets current industry standards but also anticipates emerging machining challenges.
Key Features
- Cobalt steel core delivers exceptional hardness and wear resistance for prolonged tool life.
- TiN coating reduces friction and built‑up edge, enabling higher feed rates and smoother cuts.
- Throw‑away design cuts set‑up time, allowing quick replacement and minimal downtime.
- Compact 3/4″ diameter fits standard indexable holders, ensuring easy integration on CNC and manual lathes.
- Dedicated YG‑1 support provides technical assistance, spare‑part availability, and machining guidelines.
FAQ
What materials can the YG-1 S061 insert machine?
The insert is designed for high‑nickel alloys such as Inconel, Hastelloy, and Monel, as well as stainless steels and hardened carbon steels with Brinell hardness above 280.
How often should the insert be replaced?
Because it is a throw‑away insert, it should be replaced once visible wear or coating degradation is observed, typically after a few hundred machining cycles depending on material hardness and cutting conditions.
Can the insert be used in both CNC and manual lathes?
Yes, the S061’s standard indexable shank dimensions allow it to be mounted in both CNC turning centers and manual turret lathes with compatible tool holders.
What are the recommended cutting speeds for Inconel?
For Inconel 718, a cutting speed of 120 m/min with a feed rate of 0.002 in/rev and a coolant flow of at least 10 L/min is recommended to achieve optimal performance.




 Danish Language Fiction eBook by Lindhardt og Ringhof
 Danish Language Fiction eBook by SAGA Egmont
Reviews
There are no reviews yet.